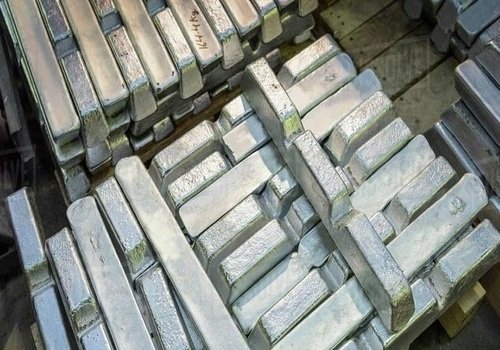
High-Purity Aluminium Ingots
Primary aluminium (P1020, 99.7% minimum) and casting alloy ingots (ADC12, LM6, LM24, A356) for die casting, electrical conductor rod and extrusion billets.
-
✓
Indian standard: IS 617 (LM6, LM24)
-
✓
European standards: EN 1676 (alloyed ingots), EN 576 (unalloyed ingots)
-
✓
Japanese and American standards: JIS H5302 (ADC12), ASTM B179 (casting alloy ingots, A356)
-
✓
Form: notch-bar ingots, 6.5 to 10 kg, and sow blocks, 500 to 750 kg
Manufacturing Process
Four steps of refining, fluxing and filtration for clean, low-dross ingots.
Primary metal and alloy selection
LME-grade primary aluminium (P1020) or clean sorted scrap is checked for low iron and silicon.
Furnace melting
Melted under strict temperature control in gas-fired or electric furnaces, then alloyed with silicon, copper and magnesium.
Degassing and filtration
Nitrogen or argon purging removes hydrogen. The melt then passes through ceramic foam filters to remove inclusions.
Continuous casting
Refined metal is cast in water-cooled steel moulds into smooth notch-bar ingots, strapped in 1 tonne export bundles.
Technical Specifications & Data Sheets
Comprehensive chemical composition limits, physical constants, and mechanical properties of pure aluminium and popular casting alloys.
1. Chemical Composition Analysis (Values in %)
| Grade | Reference | Si | Fe max | Cu | Mn max | Mg | Zn max | Ni max | Al |
|---|---|---|---|---|---|---|---|---|---|
| P1020 | EN 576 | 0.10 max | 0.20 | 0.01 max | 0.01 | 0.01 max | 0.03 | None | 99.70 min |
| ADC12 | JIS H5302 | 9.6 to 12.0 | 1.30 | 1.5 to 3.5 | 0.50 | 0.30 max | 1.00 | 0.50 | Balance |
| LM6 | BS 1490, IS 617 | 10.0 to 13.0 | 0.60 | 0.10 max | 0.50 | 0.10 max | 0.10 | 0.10 | Balance |
| LM24 | BS 1490, IS 617 | 7.5 to 9.5 | 1.30 | 3.0 to 4.0 | 0.50 | 0.30 max | 3.00 | 0.50 | Balance |
| A356 | ASTM B179 | 6.5 to 7.5 | 0.20 | 0.20 max | 0.10 | 0.25 to 0.45 | 0.10 | None | Balance |
2. Typical Physical and Mechanical Properties
| Property | P1020 | ADC12 | LM6 | A356 (T6) |
|---|---|---|---|---|
| Tensile strength (MPa) | 70 to 90 | 310 | 190 to 230 | 290 |
| Yield strength (MPa) | 30 | 160 | 90 | 220 |
| Elongation (% min) | 25 to 30 | 1.0 to 3.5 | 5.0 to 10.0 | 6.0 to 10.0 |
| Brinell hardness (HB) | 20 to 25 | 80 to 90 | 55 to 65 | 80 to 90 |
| Melting range (°C) | 660 | 515 to 580 | 570 to 580 | 555 to 615 |
| Density (g/cm³) | 2.70 | 2.74 | 2.65 | 2.68 |
3. Packaging and Ingot Dimensions
| Ingot type | Weight | Size (L × W × H) | Bundle weight | Packaging |
|---|---|---|---|---|
| Notch-bar ingot | 6.5 to 10 kg | 680 × 100 × 80 mm | 1000 kg (1 tonne) | Steel strapped, wooden pallet |
| Sow block | 500 to 750 kg | 900 × 500 × 450 mm | 500 to 1500 kg | Bare block, forklift pocket base |
Where it is used
Key downstream manufacturing sectors reliant on primary pure and alloy aluminium ingots.
Automotive engine and die casting
ADC12 and LM24 for pressure die casting of engine blocks, cylinder heads, gearboxes and crankcases.
Electrical power conductors
P1020 is remelted for overhead AAC and ACSR power line conductors and busbars.
Marine and general castings
A356 and LM6 give strength and corrosion resistance for marine pump housings and structural castings.
Architectural extrusions
Base metal for 6063 and 6061 billets used in door and window frames and curtain walls.
Utensils and household goods
Pure aluminium is rolled into circles and sheets for cookware and appliance bodies.
Deoxidising in steel plants
Aluminium ingots, notch bars and shot are used to deoxidise liquid steel.