Threaded inserts for plastic moulding
Brass threaded inserts for rotational, injection and blow moulding. Aggressive knurling gives strong torque and pull-out resistance in thermoplastics and thermosets.
- ✓ Knurling: straight, diamond, helical / spiral, unidirectional
- ✓ Thread sizes: M1.6 to M20 | 2-56 UNC to ½″ BSW / UNC
- ✓ Material: free-cutting brass, IS 319 / C36000
- ✓ Thread quality: ISO metric 6H internal threads
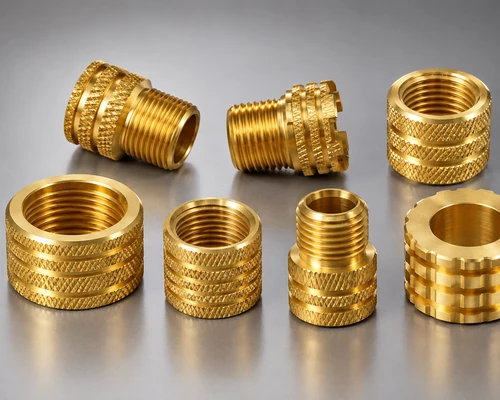
Choose a knurling pattern
| Knurling | Torque resistance | Pull-out resistance | Recommended plastics |
|---|---|---|---|
| Straight (parallel) | Moderate | High | ABS, polycarbonate, nylon (PA66) |
| Diamond (cross) | Maximum in both directions | Maximum in both directions | Polypropylene (PP), HDPE, thermosets |
| Helical (opposed) | High resistance to unscrewing | High, vibration-proof retention | PBT, PET, filled engineering plastics |
Sizes
| Thread size | Outer diameter | Length | Moulding method |
|---|---|---|---|
| Micro inserts (M1.6 to M2.5) | Ø 2.5 to 4.0 mm | 3.0 to 6.0 mm | Precision injection moulding |
| Standard inserts (M3 to M8) | Ø 4.5 to 11.0 mm | 4.0 to 15.0 mm | Injection and compression moulding |
| Heavy-duty inserts (M10 to M20) | Ø 13.0 to 26.0 mm | 12.0 to 30.0 mm | Rotational and heavy industrial moulding |
Brass Grade Table
| Grade | Standard | Copper (%) | Lead (%) | Typical use |
|---|---|---|---|---|
| IS 319 Grade 1 | IS 319, free-cutting brass | 56.0 to 59.0 | 2.0 to 3.5 | General turned parts, nuts, fittings |
| IS 319 Grade 2 | IS 319, free-cutting brass | 60.0 to 63.0 | 2.5 to 3.7 | Fast turning of fine detail |
| CW614N (CuZn39Pb3) | EN 12164 | 57.0 to 59.0 | 2.5 to 3.5 | Cable glands, inserts, fittings |
| CW617N (CuZn40Pb2) | EN 12164 | 57.0 to 59.0 | 1.6 to 2.5 | Parts that are forged then machined |
| C36000 (CW603N, CuZn36Pb3) | ASTM B16 | 60.0 to 63.0 | 2.5 to 3.7 | Terminals, pins, precision turned parts |
Primary Applications
Automotive plastic housings
Dashboard enclosures, intake manifold housings and battery terminal casings.
Consumer electronics and IT
Laptop bodies, router enclosures, smartphone test fixtures and power adapters.
Electrical enclosures
Moulded junction boxes, switch plates and circuit breaker bodies.
Press-fit and ultrasonic inserts
Brass inserts fitted after moulding by heat staking, ultrasonic vibration or cold press-fitting into pre-drilled or moulded holes in rigid thermoplastic parts, with low stress and no cracking.
- ✓ Installation: heat staking, ultrasonic vibration, cold expansion
- ✓ Head options: flanged, symmetrical (unheaded), studded
- ✓ Benefits: shorter cycle time, low stress on the plastic, clean finish
- ✓ Material: CuZn39Pb3, C36000 high-strength brass
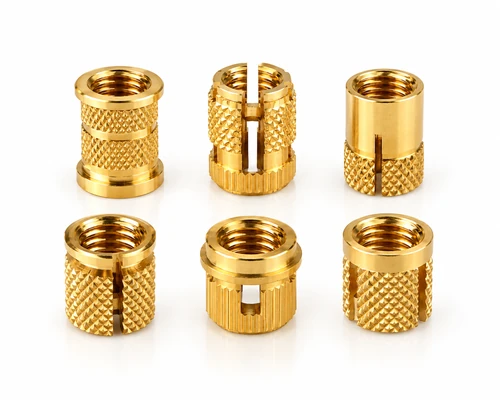
Installation methods
| Method | How it works | Retention strength | Stress on plastic |
|---|---|---|---|
| Heat staking (thermal) | The heated insert melts the plastic wall as it enters | Very high (plastic flows into the grooves) | Extremely low |
| Ultrasonic | High-frequency vibration melts the plastic around the insert | High pull-out and torque resistance | Low (cycle about 1 second) |
| Cold expansion press-fit | Pressed into the hole, then expanded by a screw drive | High initial holding power | Moderate (needs ductile plastic) |
Insert types
| Type | Shape | Benefit | Thread sizes |
|---|---|---|---|
| Flanged head | Large-diameter head flange | Stops the mating part pulling the insert through the hole | M2.5 to M10 |
| Symmetrical, unheaded | Both ends identical (entry from either end) | Suits automatic bowl feeding with no orientation check | M2 to M8 |
| Studded | External threaded male pin | No separate mating screw or bolt needed | M3 to M8 male studs |
Brass Grade Table
| Grade | Standard | Copper (%) | Lead (%) | Typical use |
|---|---|---|---|---|
| IS 319 Grade 1 | IS 319, free-cutting brass | 56.0 to 59.0 | 2.0 to 3.5 | General turned parts, nuts, fittings |
| IS 319 Grade 2 | IS 319, free-cutting brass | 60.0 to 63.0 | 2.5 to 3.7 | Fast turning of fine detail |
| CW614N (CuZn39Pb3) | EN 12164 | 57.0 to 59.0 | 2.5 to 3.5 | Cable glands, inserts, fittings |
| CW617N (CuZn40Pb2) | EN 12164 | 57.0 to 59.0 | 1.6 to 2.5 | Parts that are forged then machined |
| C36000 (CW603N, CuZn36Pb3) | ASTM B16 | 60.0 to 63.0 | 2.5 to 3.7 | Terminals, pins, precision turned parts |
Primary Applications
3D-printed assemblies
Heat-set inserts for PLA, ABS, PETG and nylon prototypes.
Medical equipment housings
Sterilizable plastic casings that are taken apart often.
Aerospace and drone frames
Lightweight carbon-filled polymer bodies that need high-torque fasteners.