High-Performance Arsenical copper alloy (C14200)
Phosphorus-deoxidised arsenical copper for parts that run hot under load, such as boiler stay bolts, firebox parts and heat exchangers.
-
✓
Indian standard: IS 288 (arsenical copper rods)
-
✓
American standards: ASTM B111, UNS C14200 (DPA grade)
-
✓
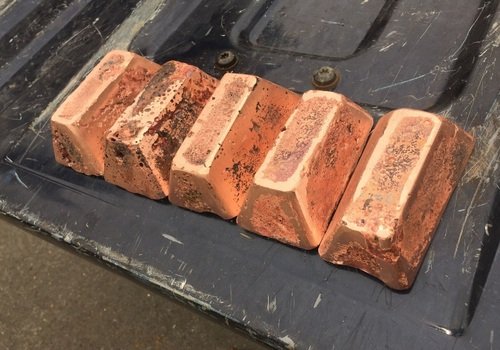
Form: ingots and billets
-
✓
Safety: not for drinking water or food contact. Safety Data Sheet on request.
Manufacturing Process
Four controlled steps to a uniform arsenical copper.
Raw material
Pure copper cathode (99.9% Cu) and clean copper scrap are selected and pre-heated to remove moisture.
Melting
Medium-frequency induction furnaces under a charcoal cover limit oxygen pick-up.
Alloying
Arsenic (0.15% to 0.50%) is added and the melt is deoxidised with phosphorus. Chemistry is checked before pouring.
Casting
Water-cooled moulds produce dense ingots and billets.
Technical Specifications & Data Sheets
Chemical composition standards, thermal limits, and physical properties of Arsenical Copper Alloy.
1. Chemical Composition Analysis
| Alloy | UNS | Copper (%) | Arsenic (%) | Phosphorus (%) |
|---|---|---|---|---|
| Arsenical copper (DPA) | C14200 | 99.40 min (with As and P) | 0.15 to 0.50 | 0.015 to 0.040 |
2. Physical Properties
| Property | Value |
|---|---|
| Electrical conductivity | About 45% IACS |
| Thermal conductivity at 20 °C | About 190 W/m·K |
| Density | 8.94 g/cm³ |
3. Packaging & Supply Specifications
| Product | Weight | Size | Bundle | Packaging |
|---|---|---|---|---|
| Ingots and billets | 20 to 35 kg | 600 × 100 × 75 mm | 1000 kg | Steel strapped pallet |
Where it is used
Key global industrial applications for High-Performance Copper Arsenic Alloys.
Locomotive and industrial boilers
Stay bolts, firebox plates and steam parts under constant heat and stress.
Heat exchangers
Shells and tubes for heat transfer duty.
Chemical processing
Evaporators, reaction kettles and acid-handling lines that need thermal efficiency.
Sugar mills and distilleries
Evaporator tubes, distillation columns and heat exchangers.